Heat Behavior at the Wall and Paper Behind the Metal: Two Practical Questions in Titanium Kettle Sourcing
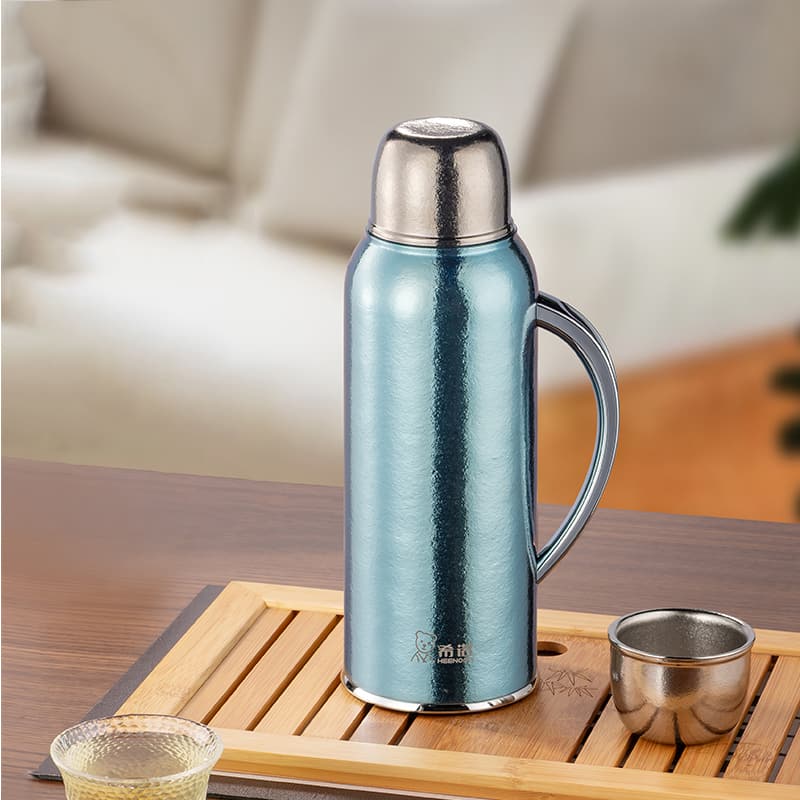
A tester holding a freshly poured Pure Titanium Fragrant Stewing Teakettle noticed the wooden handle stayed cool to the touch even after the kettle had been sitting directly on a gas burner for several minutes, while the metal body near the base was warm enough to require caution. That gap in surface temperature wasn't accidental — it's the direct result of how the kettle was designed around titanium's heat-transfer behavior, and it points to a broader question in sourcing these products: how conductivity shapes design choices like handle material and spout geometry, and separately, how a buyer actually confirms the titanium sheet used in a Titanium Vacuum Kettle is what the supplier claims it to be, rather than a lower-purity blend passed off under a standard grade label.
Why Titanium's Conductivity Changes Where Heat Shows Up
Titanium conducts heat at roughly 17 W/m·K, close to stainless steel's 16 W/m·K on paper, but the practical effect in kettle design comes less from the raw conductivity number and more from how thin titanium components typically run compared to stainless equivalents, combined with the fact that a pure titanium kettle body is meant to go directly onto an electric ceramic stove or open gas flame rather than sitting inside an outer heating element. A Titanium Vacuum Kettle body is often formed at 0.3–0.4mm wall thickness to keep overall weight down, and a thinner wall transfers surface heat toward contact points — handle, spout, lid knob — faster than a thicker stainless wall would. On a product meant for direct stovetop heating, this heat migration happens even faster than in a kettle heated indirectly, since the base is in constant contact with an open flame or ceramic element rather than hot liquid alone.
The typical design response isn't switching alloys but adjusting materials and geometry at the contact zones. A removable wooden handle addresses this directly — wood has a thermal conductivity roughly a thousand times lower than titanium, so mounting the handle as a separate, detachable wood component rather than an all-metal welded piece keeps the grip point cool even when the kettle body itself is hot from direct flame contact. The removable design also serves a second purpose beyond thermal isolation: it lets the wooden component come off before the kettle goes onto an open burner, avoiding scorching, and reattach for pouring and carrying once the kettle is off heat.
Spout geometry follows a similar logic. An eagle-mouthed spout — narrower and more angled than a straight-cut spout — is shaped to control flow velocity as water exits, reducing splashing and giving a steadier pour without needing a secondary strainer or flow restrictor. This spout profile also happens to reduce the amount of metal surface near the pouring hand, which matters slightly for heat exposure during pour, though its primary purpose is flow control rather than thermal management. Heenoor Co., Ltd. treats handle detachment mechanisms and spout profile together as part of the same design pass for stovetop-rated titanium kettles, since a spout redesigned for pour control without reconsidering handle heat isolation would only solve half the usability problem.
| Design Element |
Function |
Why It Matters for Direct-Flame Use |
| Removable wooden handle |
Thermal isolation from the metal body |
Keeps grip point cool despite direct stovetop heating |
| Eagle-mouthed spout |
Controls water flow velocity during pour |
Reduces splash without added strainer components |
| Thin titanium wall (0.3–0.4mm) |
Weight reduction |
Requires compensating handle and contact-point design |
Verifying What's Actually in the Titanium Sheet
A supplier listing "pure titanium" or "Grade 1 titanium" on a spec sheet is making a claim that's easy to state and not always easy to confirm without documentation. Commercially pure titanium is graded 1 through 4 based on oxygen and iron content, with lower grades being softer and more ductile and higher grades carrying more strength but reduced formability — a distinction that matters for something like a Pure Titanium Steeping Pot with Tea Separation Infuser, where the infuser mesh needs enough ductility to form fine perforations without cracking, while the outer body may call for a slightly higher grade for structural rigidity under repeated direct-flame heating.
Mill certificates from the titanium sheet or coil supplier list actual chemical composition by batch, and cross-checking the batch number on a certificate against the material used in a specific production run is the most direct verification path, though it only works if the kettle manufacturer maintains batch-level traceability from raw sheet to finished product. Beyond paperwork, third-party X-ray fluorescence testing on a sample coupon gives an independent composition reading, confirming oxygen and iron levels against the claimed grade rather than accepting a supplier's stated spec at face value. One practical detail worth noting for pure titanium kettles specifically: because the body doesn't require spray paint or an external coating to resist corrosion, the raw metal surface itself is directly exposed to inspection and testing, which actually simplifies verification compared to a coated product where the surface treatment would need to be stripped or bypassed before testing the base metal.
Heenoor Co., Ltd. maintains batch traceability from titanium sheet sourcing through to finished Titanium Vacuum Kettle production, giving procurement teams a documented path to verify grade claims against the specific material lot used in their order rather than relying on a general material description on the quotation.
| Verification Method |
What It Confirms |
Limitation |
| Mill certificate cross-check |
Chemical composition of the specific sheet batch |
Requires traceability records from the manufacturer |
| Third-party XRF testing |
Independent oxygen and iron content readout |
Adds cost and lead time to the verification process |
| Direct surface inspection |
Simplified due to no spray-paint coating on the body |
Still requires lab equipment for precise composition data |
Where Thermal Design and Material Verification Intersect
These two considerations aren't unrelated in practice. The thinner wall gauge that makes titanium's heat-transfer behavior a design factor in the first place also depends on using the correct titanium grade — a lower grade than specified can behave differently under stamping pressure, producing wall thickness variation that then compounds the heat-arrival issue at the handle mounting point and spout base. A Titanium Vacuum Kettle Manufacturer working with verified, traceable titanium sheet is generally better positioned to hold consistent wall gauge across a production run, which in turn keeps the removable handle fit, spout flow behavior, and unpainted surface finish on products like the Pure Titanium Fragrant Stewing Teakettle performing as designed rather than drifting batch to batch.

 English
 中文简体
 日本語
 Español
 عربى
 Vacuum Flask/Water Bottle