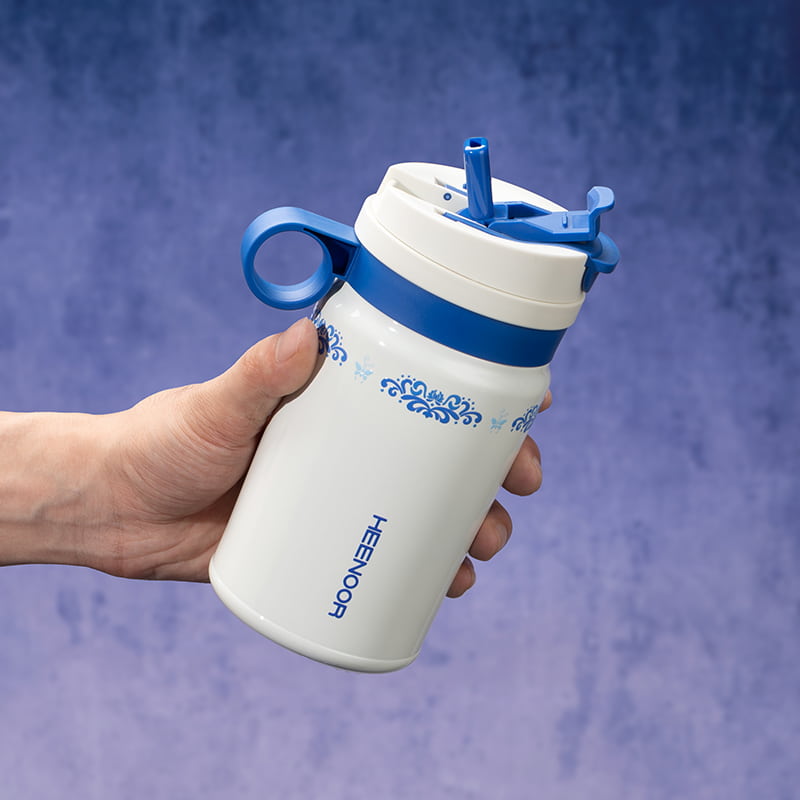
Why Heat Retention Varies So Much Across Plastic, Glass, Stainless Steel, and Titanium
A customer comparing a plastic tumbler against a stainless steel Vacuum Flask often expects the difference to come down to wall thickness alone, but the actual gap in heat or cold retention traces back to how each material conducts and radiates thermal energy at a molecular level, long before insulation structure even enters the picture.
Plastic and Glass Rely on Conduction Resistance Rather Than Vacuum
Plastic, being a poor conductor by nature, slows heat transfer simply through the resistance of its molecular structure, which is why a single-wall plastic cup can feel less scalding to hold than a metal one even without any insulation layer. The trade-off is that plastic has no mechanism to actively retain heat over time — once thermal energy moves through the wall, it dissipates into the surrounding air fairly quickly. Glass behaves similarly in that it lacks a built-in insulation structure, but its higher density and different molecular bonding give it a slower rate of heat transfer than thin plastic, which is part of why a glass cup can keep a beverage warm slightly longer during short-term use, even though neither material comes close to matching a vacuum-insulated design.
Stainless Steel and Titanium Depend on Structure, Not Just Material
A stainless steel or titanium Vacuum Flask achieves heat retention through an entirely different mechanism — an evacuated cavity between two metal walls that removes the air responsible for convective heat loss, leaving only radiant heat transfer to manage. Stainless steel, despite being a metal and therefore a natural conductor, performs well in this application precisely because the vacuum gap eliminates most conductive pathways between the inner and outer walls. Titanium follows the same structural principle but starts from a lower base density, which means a titanium-bodied bottle can achieve comparable retention performance at a reduced overall weight, a detail that matters more to buyers targeting outdoor or travel-oriented product lines than to those focused purely on desk or home use.
| Material |
Primary Retention Mechanism |
Typical Application Focus |
| Plastic |
Low thermal conductivity, no vacuum layer |
Daily carry, short-duration use |
| Glass |
Moderate conduction resistance |
Home or office, visual clarity priority |
| Stainless steel |
Vacuum-sealed double wall |
Outdoor use, extended retention needs |
| Titanium |
Vacuum-sealed double wall, lower density |
Lightweight carry, premium positioning |
What buyers often overlook is that retention performance on a spec sheet — a claim like twelve hours hot, twenty-four hours cold — depends heavily on ambient testing conditions and fill volume, which is why two products with identical vacuum gap dimensions can report different numbers depending on how the test was conducted. Heenoor Co., Ltd. tests retention performance across its material range under matched conditions specifically to keep comparisons meaningful across a Vacuum Flask and Water Bottle product line that spans four distinct material categories.
Keeping Quality Standards Aligned Across Four Different Material Processes
Running plastic injection molding, glass forming, stainless steel deep drawing, and titanium stamping under one roof creates a coordination challenge that single-material factories never have to deal with — each process has its own failure modes, its own inspection criteria, and in some cases its own regulatory reference points, yet a buyer purchasing a mixed-material product line expects one consistent quality experience across all of it.
Process-Specific Standards Cannot Be Forced Into One Template
A defect classification system built around metal forming — dents, weld porosity, thickness deviation — simply does not translate to glass, where the concerns shift toward bubble inclusion, annealing stress, and rim chip risk. Plastic introduces its own set of variables, including flow line marks, sink marks from uneven cooling, and material consistency between resin batches. Rather than applying a single inspection checklist across all four material lines, quality teams typically maintain separate criteria documents per process while aligning them under a shared severity classification — critical, major, minor — so that a defect rated "major" in glass carries the same practical weight as a "major" defect in stainless steel, even though the underlying issue looks nothing alike.
Cross-Process Coordination at the Design Stage
Consistency issues most often surface not during production but earlier, at the design handoff stage, when a product line spans multiple materials and each version needs to meet the same functional spec despite being formed through different tooling. A lid designed to fit a stainless steel bottle neck does not automatically fit a titanium version formed to a slightly different tolerance, even when both are nominally the same diameter. Heenoor Co., Ltd. addresses this by keeping tooling development and engineering validation within the same operational framework across material types, which reduces the disconnect that can occur when different processes are managed as separate, loosely coordinated production silos.
| Process Line |
Primary Quality Risk |
Verification Method |
| Plastic injection |
Sink marks, resin batch variation |
Visual inspection, batch traceability records |
| Glass forming |
Bubble inclusion, rim chip risk |
Optical inspection, thermal shock sampling |
| Stainless steel forming |
Weld porosity, wall thickness deviation |
Ultrasonic gauge, leak testing |
| Titanium forming |
Springback variation, fit tolerance |
Matched-fit sampling, dimensional grid check |
Shared Documentation Rather Than Shared Procedures
Trying to force identical procedures across chemically and structurally different materials tends to produce checklists that fit none of them well. A more workable approach keeps procedures separate but standardizes the documentation format — inspection frequency, sample size, escalation path for a failed batch — so that a procurement team auditing the factory sees a consistent reporting structure regardless of which material line they are reviewing. This distinction between shared documentation and shared procedure is often what separates a factory that manages multi-material production coherently from one that simply operates several unrelated product lines under a single company name, and it is a point Heenoor Co., Ltd. raises directly with clients evaluating a Vacuum Flask or Water Bottle program that spans more than one material category.

 English
 中文简体
 日本語
 Español
 عربى
 Vacuum Flask/Water Bottle